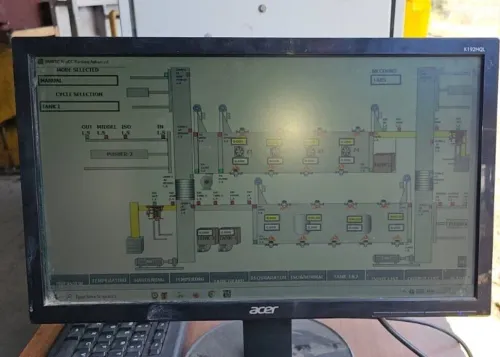

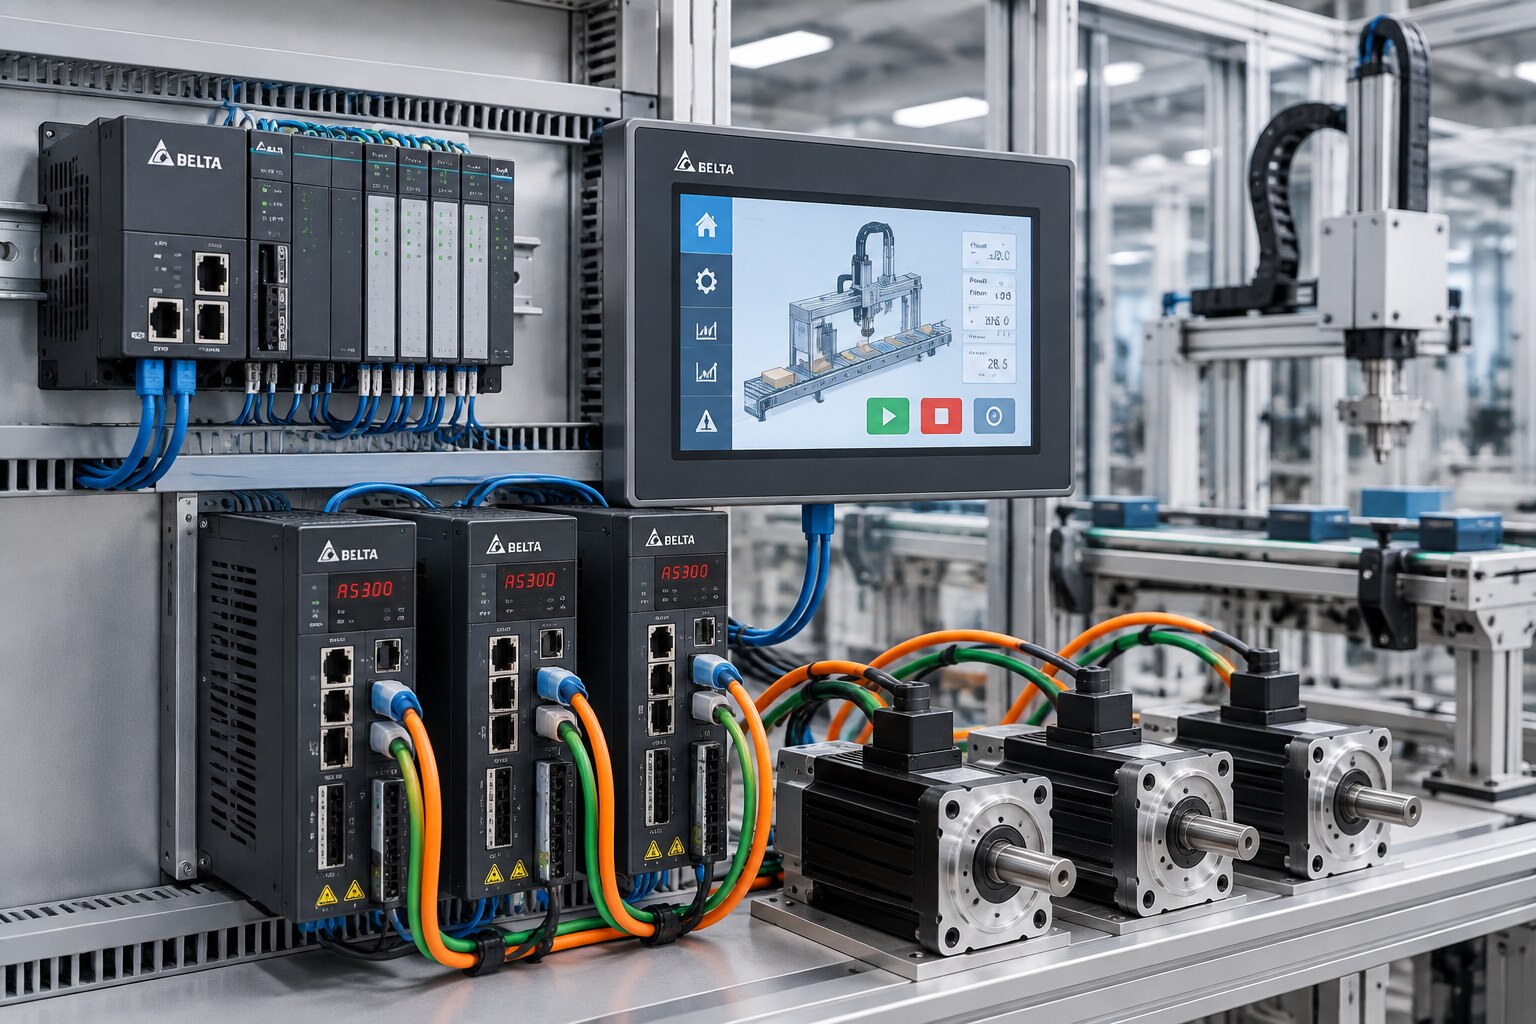
A Delta machine is not a collection of isolated parts: the PLC sequences logic, the HMI presents control and alarms, the servo executes accurate motion, and SCADA records and supervises the process. By the end, you will be able to match each component to the machine’s I/O, motion, communications, data, environmental and maintenance requirements, then define a testable Dubai project scope.
Key takeaways
- Match the PLC CPU to I/O count, motion axes, scan time and communication needs.
- Use documented tag names, alarm priorities and fail-safe states between Delta HMI and PLC.
- Size servos from torque, speed, inertia, duty cycle and braking requirements.
- Define SCADA tags, historian retention, user roles, backups and network boundaries before quotation.
How the PLC, HMI, servo and SCADA form one control system
The control system works as a closed loop: sensors report conditions, logic makes decisions, motion hardware moves the machine, and operating data returns for supervision. For a Delta industrial automation PLC in Dubai, the division of work is usually:
- PLC: reads inputs, runs the sequence, checks interlocks and commands outputs.
- HMI: presents status, alarms, settings and recipes, then sends authorised commands to the PLC.
- Servo drive and motor: convert motion commands into controlled speed, torque and position using encoder feedback.
- SCADA: collects selected PLC tags across machines, records history, displays production status and manages higher-level alarms.
The PLC remains the control authority. The HMI does not bypass its permissives, while SCADA does not replace its real-time sequence. A start command from either interface must pass the same safety, mode and process checks before the PLC enables the servo.
Motion can use pulse-train commands for straightforward positioning or a networked motion architecture for electronic gearing, camming and interpolation. Specify the method around the required synchronisation, not preference.
Test the complete chain before production:
- Simulate I/O and verify every sequence step.
- Disconnect communications and confirm the defined safe response.
- Test encoder failure, emergency stop, drive-fault reset, alarm timestamps and historian recovery.
In Dubai, include cabinet temperature, dust, ventilation and air-conditioning failure in the design; an enclosed drive cabinet can trip on heat despite a correctly calculated electrical load.
Choosing the Delta PLC family and CPU
Start with the machine’s control burden, not its digital I/O total. A compact DVP controller suits a standalone machine with modest expansion and straightforward sequencing. Choose AS for larger systems, distributed I/O or integrated motion, and AH when controller capacity, networking and future expansion justify a higher-tier platform.
A fast scan does not compensate for poor task structure or heavy communications traffic.
| Family | Choose it for | Check before ordering |
|---|---|---|
| DVP | Compact machines, basic sequencing and cost-sensitive control | CPU output type, I/O expansion, analogue modules, Ethernet port and pulse-train axis count |
| AS | Larger I/O systems, networked machines and coordinated motion | CPU scan capacity, EtherCAT or other motion network, communication modules and expansion limits |
| AH | High-capacity control, extensive networking and complex line architecture | Rack arrangement, redundancy needs, remote I/O, firmware compatibility and spare capacity |
For a Delta industrial automation PLC in Dubai, count analogue channels and motion axes separately from digital points. Select transistor outputs for pulse positioning; confirm whether the ASDA drive uses pulse, analogue or networked control. Networked motion is the better fit for electronic gearing, camming and interpolation.
Ask a Delta PLC supplier in Dubai to quote the exact CPU, modules, firmware and programming software. Require native WPLSoft or ISPSoft project files, passwords, backups and a documented spare-I/O percentage before approval.
Designing Delta HMI and PLC communications that operators can trust
Connect the Delta HMI to the PLC through a defined Ethernet or serial protocol, not an improvised cable and default driver. Specify the PLC model, HMI driver, IP addresses or node numbers, port settings, firmware versions, register map, polling rate and write permissions. A Delta HMI and PLC in Dubai installation needs documented tag ownership.
Specify each tag with a name, data type, PLC address, engineering unit, scaling, read/write status and failure value. Build the screen around these points:
- Alarms: define priority, deadband, acknowledgement, shelving, first-out capture and event timestamp; repeated messages must not hide the initiating fault.
- Recipes: identify product fields, permitted ranges, revision numbers, user permissions and download confirmation.
- Trends: state sample interval, displayed range, historian retention and behaviour during communication loss.
- Access: use individual accounts, role-based permissions, automatic logout and an audit trail for setpoint or recipe changes.
- Communications: show a clear link-status tag, freeze unsafe commands, mark stale values and place the machine in a defined safe state when the PLC link fails.
Test the complete sequence at factory acceptance: simulate I/O, disconnect and restore communications, verify alarm timestamps, test drive faults and confirm recovery from a known-good backup.
Sizing and commissioning Delta servo automation
A Delta servo is the better choice when the axis needs closed-loop positioning, rapid acceleration, repeatable indexing, electronic gearing, camming or coordinated interpolation. An AC drive suits speed and torque control; a stepper suits low-cost, lower-duty positioning; a pneumatic actuator suits simple end-to-end movement.
| Option | Best fit | Main limitation |
|---|---|---|
| Delta servo | Accurate, dynamic motion with encoder feedback | Higher cost and commissioning effort |
| AC drive | Continuous motor speed or torque control | No precise position control without added feedback |
| Stepper | Short, light-duty indexing | Can lose synchronism under overload |
| Pneumatic actuator | Fast two-position movement | Poor intermediate positioning and variable compliance |
Select pulse-train or analogue control for straightforward axes; use networked motion when synchronization, electronic gearing or interpolation matters. Do not size from motor power alone: calculate reflected inertia, peak torque, acceleration time, duty cycle, vertical load and regeneration energy, then check the drive’s overload rating and braking resistor.
Commissioning delta servo automation in dubai with this sequence:
- Confirm coupling alignment, backlash, cable shielding, encoder direction and mechanical stops.
- Set homing direction, sensor edge, offset and low-speed approach; record repeatability at production speed.
- Tune with the actual load, stiffness and speed, then test positioning accuracy, following error and settling time.
- Size braking hardware for deceleration energy. Treat a motor holding brake as load holding, not as the normal stopping device.
Test communication loss, encoder failure, emergency stop, drive reset and repeated cycles before handover.
Defining Delta SCADA scope, integration and cybersecurity
A Delta HMI serves the machine operator at the panel; a SCADA system supervises several machines, stores data and serves multiple authorised clients. Delta SCADA solutions in Dubai should therefore specify tag capacity, client/server topology, historian retention, alarm and event records, user roles, licensing and redundancy instead of treating “SCADA” as a larger HMI.
| Function | HMI | SCADA |
|---|---|---|
| Scope | One machine or cell | Line, plant or multiple sites |
| Data | Live values and short trends | Live values, historian and reports |
| Users | Local operators | Operators, supervisors, engineers and administrators |
| Access | Panel connection | Managed workstation or web client access |
| Records | Current alarms | Alarm history, events, acknowledgements and audit trail |
Specify these items before quotation:
- Tags: PLC addresses, calculated tags, alarm limits, deadbands, engineering units, scan rates and quality states.
- Historian: sampled tags, exception or periodic logging, retention period, database size, time synchronisation and recovery after storage failure.
- Protocols: Modbus TCP, Modbus RTU, OPC UA or gateway links, including register maps, byte order, polling timeouts and retry rules.
- Security: individual accounts, least-privilege roles, strong authentication, audit logs, controlled industrial firewall or VPN, and no PLC or SCADA port exposed directly to the internet.
- Resilience: server redundancy, UPS-backed network equipment, scheduled offline backups, tested restore procedures and change-controlled software images.
Remote support must not weaken production availability. Test communication loss, historian recovery and restoration from a known-good backup during acceptance.
Planning a Dubai project from quotation to handover
A low quotation is not comparable until it names the exact Delta PLC family, CPU, communication modules and firmware. Ask each Delta PLC supplier in Dubai to state I/O capacity, motion functions, programming software, panel components, commissioning hours, spares and exclusions.
| Supplier evidence | What to require | Why it matters |
|---|---|---|
| Controller | Exact DVP, AS or AH part number and firmware | Similar-looking CPUs can change software and protocols |
| SCADA | DIAView version, driver, OPC, SQL and third-party licences | Connectivity depends on version and licensed modules |
| RS-485 | Baud rate, parity, station address, register map, byte order, master role, retries and timeout | Wrong offsets cause faults blamed on the HMI |
| Servo | Motor, drive, encoder, brake, homing method and tested load | Resolution does not remove backlash or coupling error |
Check the Dubai installation for cabinet heat, dust, humidity, condensation, cable routing, earthing, voltage quality and air-conditioning. Separate remote-support availability from internet exposure: use an industrial firewall or VPN, individual accounts, least privilege, backups and change logs.
Before cutover, run a proof of concept with the actual PLC firmware, network topology and DIAView licence. Factory and site tests must include:
- I/O simulation and the complete production sequence
- Communication loss and restoration
- Sensor or encoder failure, emergency stop and drive-fault reset
- Alarm timestamps, historian recovery and backup restoration
- Servo repeatability, homing and positioning at production speed and load
IkodeAutomation |08048033508 can be evaluated against this evidence rather than catalogue breadth.
Related products
 | Component Sales and Services Delta Industrial Automation Ikodeautomation is one of the best Delta Industrial Automation solution providers, offering Delta PLC, HMI, Servo, SCADA, AC Drives and complete... View product → |
 | Industrial Automation Solutions & System Integration PLC Control Panel Manufacturer & Automation Solutions Professional PLC Control Panel Design & Automation Solutions -Ikodeautomation provides professional PLC Control Panel design, manufacturing,... View product → |
Frequently asked questions
How do the PLC, HMI, servo and SCADA form one control system?
The PLC reads sensors and executes control logic, the HMI presents machine status and commands, servo drives control motion, and SCADA supervises production data, alarms and trends.
How do you choose a Delta PLC family and CPU?
Compare the required digital and analogue I/O, scan time, motion-axis count, memory, expansion modules and communication protocols before selecting the CPU.
How do you make Delta HMI and PLC communications reliable?
Use a documented tag list, consistent data types, defined equipment states, alarm priorities, communication-loss handling and tested operator permissions.
What information is needed to size Delta servo automation?
Provide the load mass, mechanical transmission, travel distance, target speed, acceleration, duty cycle, stopping time, inertia and required positioning accuracy.
What should a Delta SCADA project include?
Define screens, tags, alarm rules, trends, historian retention, reports, user roles, backups, network segmentation and connections to other systems.
Related products
 | Industrial Automation Solutions & System Integration PLC Programming Services Professional PLC Programming & Automation Solutions - Ikode Automation is one of the best PLC programming and industrial automation solution... View product → |
 | Industrial Automation Solutions & System Integration HMI Programming Services Ikodeautomation is one of the best HMI programming and industrial automation solution providers, offering professional HMI development and PLC-HMI... View product → |
 | Industrial Automation Solutions & System Integration Industrial Automation Component Sales Reliable Automation Components. Trusted Industrial Solutions.Ikodeautomation is one of the leading industrial automation component sellers and... View product → |
 | Industrial Automation Solutions & System Integration PLC Integration & Industrial SCADA SCADA Development Services Industrial SCADA Solutions by Ikodeautomation is one of the leading choices for SCADA development and industrial automation solutions, providing... View product → |