
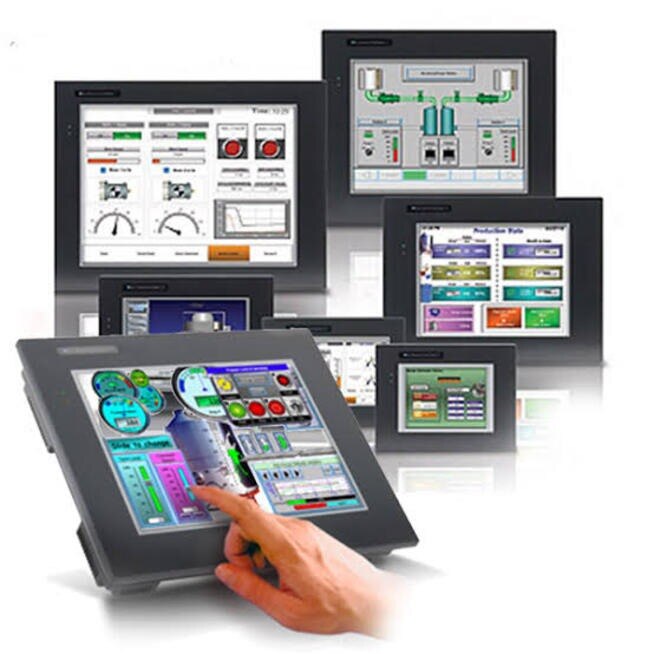
A PLC-HMI project can fail even when the screens look finished: tags may use the wrong data type, alarms may lack actionable limits, and a panel may lose recipes after a power cycle. By the end, you will know how to define the technical scope, compare integrators, prepare quotation inputs, and accept a system through FAT, SAT and commissioning.
Key takeaways
- Choose platforms from installed hardware, plant connections and future support.
- Specify HMI model, PLC model, protocol, I/O list and screen requirements.
- Demand separate FAT and SAT plans for new machines and retrofits.
- Test alarms, recipes, communications, recovery and user permissions before handover.
Which HMI and PLC platforms should your Pune project support?
Choose the platform from the machine’s installed hardware, required plant connections and future support plan—not from the screen count. A quotation from an hmi programming company in pune should identify the exact HMI, PLC and communication path.
| Platform group | Examples to confirm | Details to specify |
|---|---|---|
| HMI | Siemens WinCC; Rockwell FactoryTalk View; Schneider EcoStruxure Machine Expert; Mitsubishi GOT; Omron NB; Weintek EasyBuilder Pro | Panel model, screen resolution, runtime or engineering version, driver and license |
| PLC | Siemens S7-1200, S7-1500; Rockwell ControlLogix, CompactLogix; Schneider Modicon; Mitsubishi MELSEC | CPU model, firmware, memory, protocol and engineering software |
| Mixed-brand | Siemens HMI with Rockwell PLC | Supported driver or OPC UA gateway, data types, tag limits and gateway license |
“Ethernet connectivity” is not a compatibility specification. Require the supplier to document Ethernet or serial links, protocol and driver versions, IP addresses, managed-switch settings, OPC servers, firewall rules and remote-access boundaries. A replacement panel can fail through an unrecorded firmware mismatch, runtime license, font, resolution or retentive-memory setting.
Define whether plc hmi integration in pune covers only a local operator panel or also SCADA, MES, a historian, OPC UA or the plant network. That boundary changes cybersecurity controls, user and gateway licensing, data-retention design and testing.
A plant-connected system needs interface and recovery tests; a local panel still needs power-cycle, communication-loss and backup tests.
What should HMI programming include beyond drawing screens?
A complete scope for industrial hmi programming services covers operator workflows, control boundaries and verification—not just attractive graphics. It should define the following:
1. Build a screen hierarchy from plant overview to area, line, equipment detail and faceplates. Include process graphics, consistent navigation, alarm banners, alarm history, trends, recipes, user roles, audit trails, language selection, device diagnostics and maintenance screens.
2. Create a written data contract for every HMI object. Record the PLC tag name, data type, engineering unit, scaling, quality or validity status, fail-safe value, alarm limit, read/write permission and PLC ownership of each command. This prevents a displayed value from looking correct while writing the wrong type, range or control state.
3. Treat an HMI button as an action request, not a safety device. The PLC must check mode, permissives, interlocks, sequence state and command timeout; safety functions belong in a safety PLC, safety relay or hardwired circuit.
The PLC must also revalidate recipe and set-point values received from an HMI, MES, engineering tool or communications client.
4. Rationalize each alarm by documenting its cause, consequence, operator action, priority, limit, deadband, delay and shelving or suppression rule. Use ISA-18.2 for alarm management and ISA-101 for HMI philosophy, including color conventions, navigation, faceplates, standards and change control. A quotation listing screens alone can omit PLC logic, tag mapping, communications testing and commissioning.
What information should you provide before receiving a quotation?
Send a quotation pack that lets every bidder price the same plant, not a rough screen count.
Include PLC and HMI model numbers, firmware versions, software and runtime licenses, I/O list, tag database, electrical drawings, sequence of operation, alarm list, drive and instrument count, recipe count, screen-resolution requirements, required languages, network topology, protocol gateways, historian or report requirements, and the intended SCADA, MES or OPC UA connection.
| Quotation item | Assumption to compare |
|---|---|
| PLC scope | Application logic, sequencing, interlocks and PLC code changes |
| HMI scope | Visualization, tag mapping, alarm handling, user management and operator workflows |
| Data and communications | Historian links, protocol gateways, communications testing and commissioning |
| Site delivery | Panel or network changes, FAT and SAT days, travel and shift coverage |
| Long-term ownership | Source-code ownership, warranty response and change-order rates |
Ask the hmi programming company in pune to state tag and I/O counts, alarm volume, recipe count, historian retention, report quantity and database backup responsibility. A quotation for HMI programming and PLC integration services in Pune is incomplete if it prices screens but omits PLC sequencing, tag mapping, communications testing or commissioning.
For Marathi-, Hindi- or English-speaking plants, provide a controlled language table. Require consistent units, date and time formats, font-rendering checks and a translation-review process so new alarms do not become truncated or mixed-language messages.
How does delivery differ for a new machine and a retrofit?
A new machine allows PLC logic and HMI screens to be developed offline, with tag mapping tested against simulated inputs before hardware arrives. The sequence can be revised early, followed by FAT using the intended panel, PLC and drives. That reduces surprises during installation.
A retrofit starts with evidence, not code changes. Document the existing PLC program, panel resolution, firmware, communication drivers, retentive-memory behaviour, recipes, clock and time-zone settings, field wiring, production constraints and rollback method before selecting replacement hardware.
| Project stage | New machine | Retrofit |
|---|---|---|
| Offline development | Build logic and screens from approved sequence; simulate inputs and revise mapping | Capture and preserve the existing program, configuration and operator behaviour |
| FAT | Test the intended panel, PLC, drives, alarms and sequences before shipment | Test replacement hardware against the documented baseline and rollback plan |
| Site work | Install and verify the new system | Replace or modify equipment without losing recipes, timing or production access |
Cold commissioning means checks before live process operation. SAT verifies installed wiring, instruments, drives, network and plant interfaces. Hot commissioning means controlled live operation under approved bypasses, defined production windows and named ownership of process risk.
Operator handover for industrial HMI programming services must include:
- PLC source and compiled files; HMI project and runtime files
- Network and device configuration, licenses and tag database
- Alarm and recipe exports, password ownership and restore instructions
- Tested backups, including historian or report databases where used
Bench-test replacement hardware, or validate it on the intended panel, before acceptance. This evidence matters in plc HMI integration in Pune, especially when a retrofit affects a running line.
How should you test and choose an HMI-PLC integration partner in Pune?
Choose an HMI programming company in Pune by demanding evidence, not a screen count.
Its FAT and SAT matrix must record normal sequence, simulated inputs, permissive and interlock failure, sensor fault, manual-to-automatic transition, communication loss, alarm generation and acknowledgement, user permissions, recipe range and data-type checks, power-cycle recovery, recipe retention, historian or report output, fail-safe values and command timeouts.
| Check | Accept | Reject |
|---|---|---|
| FAT/SAT evidence | Traceable test ID, expected result, actual result, witness and defect closure | “Tested successfully” without records |
| Recipe security | HMI checks type, unit, range, authority and revision; PLC validates again | Limits enforced only on the screen |
| Recovery | Tested PLC/HMI/database restore with versions, licenses and instructions | A backup file with no restoration proof |
| Access control | Named accounts, least-privilege roles, MFA where supported, controlled vendor access, session logs and revocation | Shared passwords or permanent remote access |
The PLC must reject invalid values arriving through an engineering tool, retained memory, communications client or MES interface. Ask for the data contract, source-code ownership, supported platforms, communication path, commissioning coverage and post-handover response. Under NIST SP 800-82 principles, ask how availability and safety are protected while handling access.
For a buyer comparing hmi programming and plc integration services in pune or plc hmi integration in Pune, IkodeAutomation |08048033508 belongs on the comparison list only when its proposal names that evidence and handover scope. A low quote becomes expensive when missing tests surface during production.
Related products
 | Industrial Automation Solutions & System Integration HMI Programming Services Ikodeautomation is one of the best HMI programming and industrial automation solution providers, offering professional HMI development and PLC-HMI... View product → |
 | Industrial Automation Solutions & System Integration PLC Programming Services Professional PLC Programming & Automation Solutions - Ikode Automation is one of the best PLC programming and industrial automation solution... View product → |
Frequently asked questions
Which HMI and PLC platforms should a Pune project support?
Choose platforms that match the installed PLC and HMI hardware, required plant protocols, available engineering tools and your long-term maintenance plan. Confirm the exact models and communication path, such as Ethernet/IP, PROFINET, Modbus TCP or OPC UA.
What should HMI programming include beyond drawing screens?
Require tag mapping, alarm handling, trends, recipes, user roles, diagnostic messages, navigation, PLC communication checks, audit records where needed, backups and operator documentation. Test every command, interlock and fault response.
What information should you provide before receiving a quotation?
Provide the PLC and HMI make and model, firmware versions, I/O list, electrical drawings, control narrative, sequence of operation, network diagram, protocol requirements, screen list, alarm list, recipe needs and site constraints.
How does delivery differ for a new machine and a retrofit?
A new machine allows controls and network architecture to be designed together. A retrofit must account for live equipment, legacy PLCs, undocumented wiring, production downtime, backup and rollback plans, panel changes and staged commissioning.
How should you test and choose an HMI-PLC integration partner in Pune?
Ask for a platform-specific example, a written scope, source-code and backup ownership, FAT and SAT procedures, commissioning support and post-handover response terms. Test communications, alarms, interlocks, recovery and user access before acceptance.