
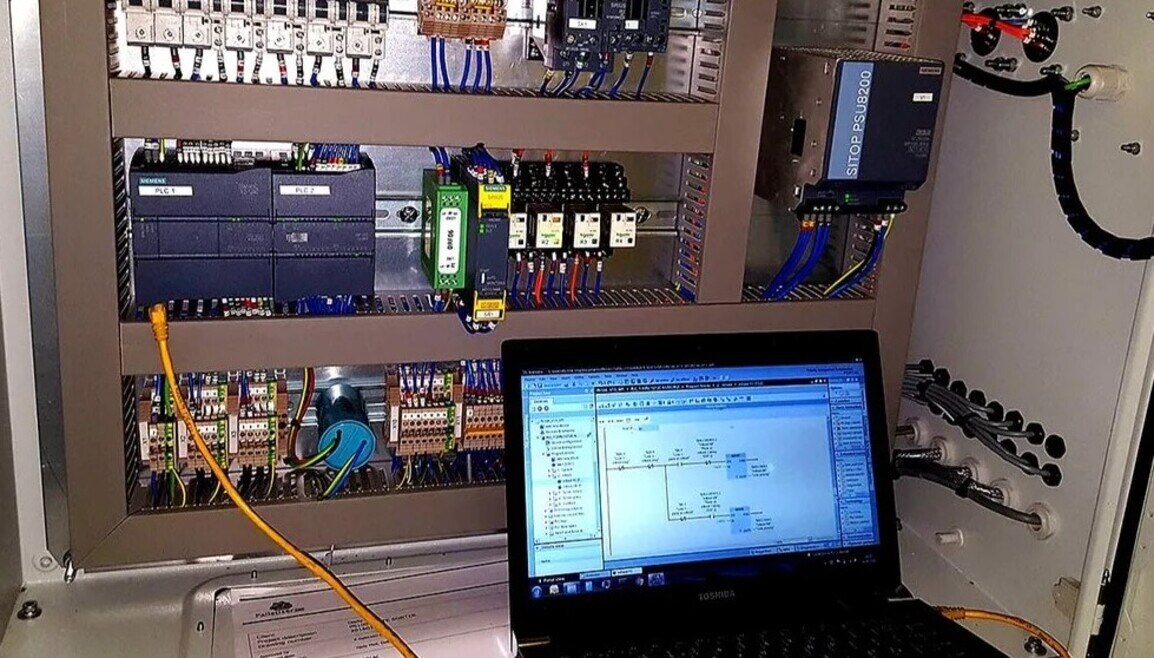
A machine can run a basic automatic cycle and still fail because its interlocks, alarms, drives, HMI tags, recovery states or documentation were never defined properly. By the end, you will know how to specify the programming job, compare providers, prepare the required machine information and judge whether the delivered system is ready for production.
Key takeaways
- Confirm the PLC family, CPU model and firmware before hiring.
- Require an I/O list, sequence description and alarm matrix before coding.
- Demand simulation, FAT, SAT and documented commissioning records.
- Include source-code ownership, backups and software licences in handover terms.
Choose the PLC platform, software environment and programming language first
Confirm the exact PLC family, CPU model and firmware before appointing a programmer.
PLC programming services in Pune should name their experience with Siemens S7-1200 and S7-1500 in TIA Portal, Allen-Bradley CompactLogix and ControlLogix in Studio 5000, Mitsubishi in GX Works, Omron in Sysmac Studio, Schneider Electric in EcoStruxure Control Expert or Machine Expert, and CODESYS-based controllers.
| Platform | Software environment | Confirm before appointment |
|---|---|---|
| Siemens S7-1200/S7-1500 | TIA Portal | CPU and firmware match |
| Allen-Bradley CompactLogix/ControlLogix | Studio 5000 | Major revision and add-on profiles |
| Mitsubishi | GX Works | CPU series and project version |
| Omron | Sysmac Studio | Controller, motion and library compatibility |
| Schneider Electric | EcoStruxure Control Expert or Machine Expert | Runtime and device libraries |
| CODESYS controllers | CODESYS | Vendor runtime and target package |
Ask which IEC 61131-3 languages the programmer supports: Ladder Diagram, Structured Text, Function Block Diagram and Sequential Function Chart. Language choice affects diagnostics, maintenance and portability; Structured Text suits calculations, while Ladder Diagram often speeds fault tracing for electricians.
Define the assignment in writing:
- New-machine PLC programming
- Code modification or troubleshooting
- PLC migration
- Complete control redesign
Industrial PLC programming in Pune must also separate standard logic from safety functions. Emergency stops, guard switches, two-hand controls and safety-related motion need a documented safety design; ordinary PLC bits do not replace a safety relay or safety PLC. IEC 60204-1 covers machine electrical equipment, protective bonding, control circuits, emergency stops, documentation and verification.
Turn the machine sequence into a complete programming specification
Before logic is written, approve a sequence-of-operations document covering idle, setup, manual, semi-automatic, automatic, hold, fault and recovery modes. Define each permissive, interlock, start condition, stop condition, alarm, reset rule, recipe value and actuator timeout. State which outputs remain energised during hold and which require a fresh start.
Define abnormal behaviour explicitly:
| Condition | Required response | Acceptance check |
|---|---|---|
| Sensor disagreement | Stop motion, raise a diagnostic alarm and require authorised recovery | Simulate conflicting inputs |
| Cylinder misses position | Remove command after timeout and block the next step | Test extended and retracted timeout |
| Low air pressure | Inhibit motion and retain the fault until pressure is restored and reset | Drop the pressure switch |
| Drive fault | Stop the affected sequence and display the drive code | Remove and restore drive-ready |
| Remote I/O loss | De-energise unsafe outputs and prevent automatic restart | Disconnect the rack |
| Communication timeout | Apply the defined safe state, retry and alarm | Break the network link |
| Power return or emergency-stop recovery | Require a deliberate reset and verified home conditions | Restart during each machine mode |
Give the machine plc programming service electrical drawings, I/O list, motor and valve data, sensor types and polarity, drive details, HMI screen list, safety-circuit description, network addresses and existing PLC backup. Include analog ranges and units, such as 4–20 mA pressure values and encoder counts.
On an existing machine, document undocumented wires and signals operators rely on; otherwise production-critical behaviour becomes guesswork.
Expect a testable workflow from I/O mapping to site commissioning
A professional PLC automation programmer proves the machine in stages, not by showing that one normal cycle runs. Require signed test records from the approved I/O map through commissioning.
1. Approve the I/O map before coding. Use consistent tag names, documented addresses and a hardware configuration matching the installed CPU, remote racks, drives and fieldbus devices.
2. Build modular logic for sequences, alarms, interlocks, recipes and HMI communication. Run offline simulation or a controlled dry run before connecting production equipment.
3. Test each function deliberately: sensor polarity, analog scaling, actuator timeouts, drive status, manual controls, alarm latching and reset permissions. A PLC automation programmer in Pune should demonstrate safe I/O forcing or simulation rather than rely on visual inspection.
4. Separate factory acceptance testing from site acceptance testing. FAT checks the programmed system in the workshop; SAT checks field wiring, network addressing, electrical noise, pneumatic response, drive tuning, operator workflow and upstream or downstream timing on the actual machine.
5. Put FAT, site installation, SAT, production ramp-up and post-commissioning support in the quotation. Acceptance must include power loss, emergency-stop recovery, communication loss, failed sensors, low air pressure and machine restart, not only the normal cycle. Record every result, failed test and unresolved deviation before handover.
Compare retrofit and recovery capability before production stops
Assess the provider by requesting a written recovery plan before production stops. It must begin with a backup of the live controller, HMI, drives and network configuration; changing logic first can destroy the only usable evidence.
- Identify the CPU, firmware revision, memory card, expansion modules, field wiring and replacement availability.
- Decide whether to restore, modify, migrate or redesign the control system.
- If source code is missing, complete a controlled I/O survey, update electrical drawings, reconstruct tags and stage testing instead of replacing everything immediately.
For obsolete hardware, compare a like-for-like repair with migration to a current platform. Calculate production downtime, spare availability, engineering effort and future support, not just the purchase price.
| Option | Strength | Check before choosing |
|---|---|---|
| External PLC programming service | Broad platform and commissioning capability | Verify matching hardware experience, safety competence and documentation |
| In-house PLC automation programmer | Fast access to your machine and process knowledge | Confirm platform skills, backup discipline and site commissioning capacity |
| Machine OEM code | Known sequence and standard libraries | Check whether the OEM still supports the hardware and can supply source files |
| Electrician changing ladder logic | Useful for wiring faults and simple edits | Reject the approach for safety logic, migrations or undocumented systems |
A credible machine PLC programming service explains its test controls and handover records. IkodeAutomation |08048033508 belongs on the shortlist only when its Pune team can show matching platform experience, a downtime plan and comparable machine references. Compare PLC programming services in Pune on those proofs, not on the promise of quick recovery.
Related products
 | Industrial Automation Solutions & System Integration PLC Programming Services Professional PLC Programming & Automation Solutions - Ikode Automation is one of the best PLC programming and industrial automation solution... View product → |
 | Industrial Automation Solutions & System Integration PLC Control Panel Manufacturer & Automation Solutions Professional PLC Control Panel Design & Automation Solutions -Ikodeautomation provides professional PLC Control Panel design, manufacturing,... View product → |
Make PLC software integration and handover part of the scope
Demand a documented interface and recovery package, not just working ladder logic. For PLC software integration in Pune, specify the exact PLC CPU and firmware, programming software version, HMI runtime, drive firmware, Ethernet or fieldbus protocol, and every third-party device file.
1. Define each connection before commissioning. State whether PLC data is exchanged cyclically for control or asynchronously for monitoring and reporting. For OPC UA, document namespaces, data types, timestamps, quality states, update rates, buffering, authentication and interface ownership. OPC UA does not automatically expose every useful tag.
If OPC UA, MQTT, a database or SCADA enters the control path, set limits for latency, packet loss and retries, then define the machine’s safe state for link failure.
2. Require a handover package containing tested PLC, HMI and drive backups; source and deployable files; hardware configuration; I/O list; network topology; alarm list; recipes; libraries; licences; access procedure; change log; and restore instructions. Industrial PLC programming in Pune is incomplete if the project opens only on one programmer’s laptop.
3. Require segmented networks, controlled remote access, least-privilege accounts and offline backups. Test restoration on a separate engineering computer, record the software and firmware versions used, and verify that the restored system communicates with drives, HMI, SCADA, MES and neighbouring machines before release.
A complete deliverable lets maintenance restore the machine without depending on one laptop or one programmer.
Frequently asked questions
How do you choose a PLC platform and programming environment?
Confirm the PLC family, CPU model and firmware first, then match the programmer’s software environment, language and required licences to that hardware.
What should an industrial machine PLC programming specification contain?
Document the operating sequence, I/O list, modes, interlocks, alarms, recipes, safety interfaces, HMI screens and abnormal-condition responses before development begins.
What testing should PLC programming services include?
Expect a workflow covering I/O mapping, offline logic checks, simulation or factory acceptance testing, panel checks, site acceptance testing and commissioning records.
What should PLC software integration and handover include?
Require tested connections to HMIs, drives, robots, databases or plant systems, plus source code, backups, version details, passwords, licences and as-built documentation.