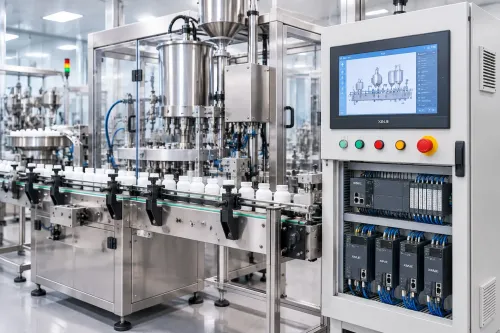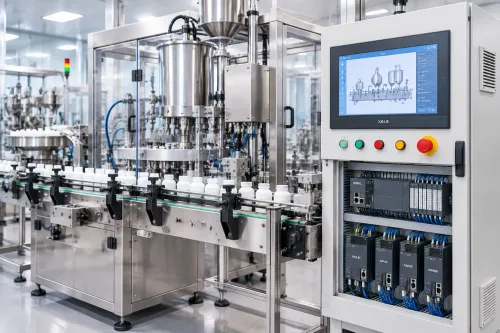

A pharmaceutical automation project needs more than a Delta PLC, HMI or servo quotation: you must match the control family, motion load, network, data architecture and validation evidence to the process. By the end, you will have a practical basis for specifying equipment, testing regulated functions and comparing a Delta PLC HMI servo supplier in Bengaluru.
Key takeaways
- Select the PLC family from I/O architecture, motion load and process-control requirements.
- Size each servo for torque, speed, inertia, duty cycle and stopping performance.
- Use the HMI for operator actions and SCADA for plant-wide supervision and records.
- Specify audit trails, user access, validation documents and hygienic hardware before procurement.
Choose the Delta PLC family from the process architecture
Select the Delta PLC family from the machine’s I/O architecture, motion workload and process-control needs—not from point count alone. For delta plc for automation pharma in bengaluru projects, a compact blister machine needs a different controller than a multi-station line or process skid.
| Family | Best fit | Selection check |
|---|---|---|
| DVP | Stand-alone machines with compact I/O and straightforward sequencing | Confirm expansion limits, scan time, positioning needs and communication modules |
| AS | Modular machines and production lines needing more I/O, networking and coordinated control | Confirm CPU capacity, motion requirements, remote-I/O architecture and firmware |
| AH | Larger, higher-end control systems with extensive expansion and demanding coordination | Confirm system architecture, controller capacity, network design, retentive memory and lifecycle support |
Use DVP when the machine has limited stations and local I/O. Choose AS when several modules, drives, HMIs or line sections must exchange status and commands. Consider AH when the control system needs substantial expansion or complex, centralised coordination.
Do not specify servo motors for every process-skid function; valves, instrumentation, proportional control and variable-frequency drives suit many dosing, mixing and temperature loops better.
Require these details in the quotation:
- Exact CPU and firmware revision
- Digital, analogue, high-speed and remote-I/O modules
- Scan-time limit and retentive-memory capacity
- Network modules and supported protocols
- Motion-axis count and update requirements
- Spare I/O, cabinet space and replacement strategy
A family choice is sound when it leaves capacity for recipe handling, alarms, interlocks and future validation changes without forcing a controller replacement.
Size servo axes and connect the control system correctly
Calculate each servo axis from the load, not the machine name. Include reflected inertia after gearbox reduction, friction torque, process torque, acceleration torque, maximum speed, acceleration time and the duty cycle. Keep the motor’s continuous RMS torque below its rated value and peak torque below its permitted limit; check the drive’s regenerative capacity during deceleration.
Use a gearbox when it lowers reflected inertia or improves resolution, then verify backlash, positioning accuracy and the inertia ratio with Delta’s sizing tool.
| Connection | Preferred use | Check before approval |
|---|---|---|
| EtherCAT | Synchronized filling, indexing, capping and pick-and-place axes | Cycle time, node addressing and cable topology |
| Modbus TCP | PLC-to-HMI, VFD and utility-device data | Register mapping, timeout handling and write permissions |
| Modbus RTU | Simple instruments or legacy drives | Termination, baud rate and unique slave addresses |
| OPC UA | SCADA or historian exchange | Tags, certificate trust and timestamp quality |
Use the PLC for sequence control, interlocks and operating parameters; keep batch records, audit trails and retention in a controlled SCADA or database layer. Configure separate engineering and operator accounts, least-privilege access, segmented OT networks, controlled USB use, restricted remote access and tested backups.
A PLC, HMI or SCADA package alone does not satisfy 21 CFR Part 11.
For Delta industrial automation in Bengaluru, test sensor disconnection, drive faults, network loss, power recovery, invalid recipes, emergency stops and interrupted-batch restarts during FAT. Verify clock synchronisation across PLC, HMI and SCADA, including time-source failure.
Define what the HMI records and what SCADA supervises
A pharmaceutical HMI should show the operator what the machine is doing and limit what the operator can change. Display batch status, equipment states, active alarms, alarm history, recipe name and version, setpoint limits, manual-mode controls, servo or drive faults, and permissive conditions.
Block a start when a guard, valve, pressure, temperature, or cleaning condition is not satisfied.
Use the HMI to control defined operating actions and capture local events:
- Record operator log-in, log-out, acknowledgements, mode changes, setpoint changes, recipe selection, and failed commands.
- Require authorised users to create, approve, download, or change recipes.
- Preserve the previous recipe value, new value, user identity, timestamp, and reason for change.
- Show the batch identifier and equipment state on every relevant operating screen.
SCADA supervises across machines and batches. It should collect historian tags, alarm and event records, batch reports, downtime data, trends, and production summaries while providing role-based access, search, reporting, backup, restore, and redundancy. Specify these functions for Delta SCADA solutions in Bengaluru; an Ethernet connection or screen list is not a SCADA specification.
Keep machine states and short-term operating parameters in PLC memory, but retain batch records, audit trails, and long-term history in a controlled SCADA database or manufacturing-execution layer. Synchronise PLC, HMI, and SCADA clocks to a controlled plant time source and test clock drift and time-source failure.
A Delta package alone does not establish 21 CFR Part 11 compliance; validated configuration, secure audit trails, electronic signatures, record protection, procedures, and documented checks do.
Build data integrity, validation and hygienic design into the specification
Treat Delta automation for pharmaceutical plants as a validated system, not a collection of stainless-steel boxes. Specify the cleanroom location, washdown exposure, enclosure IP rating, heat dissipation, hygienic cable entries, power-signal segregation and maintenance access. A high IP rating does not prove suitability for a classified area.
Put recipe control in the validation plan. Define who may create, approve, download or change a recipe; retain the old value, new value, user, timestamp and reason; block unauthorised overwriting; and test backup restoration with an actual recovery record.
Keep regulated records outside ordinary PLC memory. Use the PLC for control states and operating parameters, while a controlled SCADA, database or manufacturing-execution layer retains batch records, audit trails and historical data under documented retention, access and restore procedures. Check the exact DIAView edition and licensed modules rather than assuming they provide every regulated-data function.
Build the requirements-to-test chain before programming:
- Link the URS, functional or software specification, design documents, FAT, SAT, IQ and OQ.
- Define PQ around the process and operating procedure; a panel test alone does not demonstrate process performance.
- Provide separate engineering and operator accounts, least-privilege permissions, segmented OT networks and restricted remote access.
- Control removable media, document patch and firmware changes, and test backups.
- Record the feature matrix for audit trails, electronic signatures, historian behaviour, OPC connectivity, redundancy, directory integration and validated backup/restore.
Use cleanable surfaces, protected components and accessible service points so hygiene survives maintenance, not just commissioning.
Compare suppliers through testing, handover and lifecycle controls
Require a witnessed FAT, a repeatable SAT, complete source-code handover and a lifecycle plan before you approve any Delta PLC HMI servo supplier.
| Control | Evidence to require | Red flag |
|---|---|---|
| FAT and SAT | Approved test scripts covering I/O, interlocks, recipes, alarms, servo homing, loss of communication, power recovery and alarm-history timestamps | Demonstration only, without recorded pass/fail results |
| Software handover | Exact CPU, HMI and drive models; firmware revisions; software versions; licensed project files; source code; backups; passwords; network drawings; and an image of the engineering workstation | Supplier retains the only editable project |
| Validation support | Requirements and design traceability, FAT/SAT records, deviation log, change-control procedure and configuration baseline | “Compliant” claimed without test evidence |
| Lifecycle control | Obsolescence status, approved spare equivalents, license-renewal costs, patch procedure, restore test and remote-access approval process | Replacement parts or software compatibility left undefined |
Test the PLC, HMI, servo drives and SCADA together, including PLC/HMI/SCADA clock drift, loss of the plant time source, daylight-saving handling where applicable, and historian timestamp order. A time failure can make a batch investigation ambiguous.
Keep batch records and audit trails in a controlled SCADA, database or MES layer with retention, backup, restore and access rules; PLC memory alone is not a validated record system. Require separate operator and engineering accounts, segmented OT networking, controlled removable media and tested remote access.
21 CFR Part 11 depends on configuration, electronic signatures, audit trails and procedures—not the Delta package alone.
Ask IkodeAutomation |08048033508 to provide this evidence in the same review pack as every competing supplier.
Related products
 | Industrial Automation Solutions & System Integration Pharma Industrial Automation System Smart, Reliable & Scalable Automation for Pharmaceutical Manufacturing Ikodeautomation is one of the best industrial automation solution providers... View product → |
 | Component Sales and Services Delta Industrial Automation Ikodeautomation is one of the best Delta Industrial Automation solution providers, offering Delta PLC, HMI, Servo, SCADA, AC Drives and complete... View product → |
Frequently asked questions
How do you choose a Delta PLC family for a pharmaceutical machine?
Match the PLC to distributed I/O, motion axes, scan-time demands, communication protocols and process-control functions—not point count alone.
What factors determine Delta servo sizing for pharma equipment?
Calculate required torque, speed, reflected inertia, duty cycle, acceleration, braking and stopping performance for each axis before selecting the servo motor and drive.
What should the HMI record, and what should SCADA supervise?
Use the HMI for local operation, alarms, recipes and operator actions. Use SCADA for plant-wide status, trends, reports, user permissions and supervisory records.
What should you compare when selecting a Delta PLC, HMI and servo supplier?
Compare application testing, FAT and SAT evidence, source-code and drawings handover, validation documents, training, spare parts and lifecycle support.
Related products
 | Industrial Automation Solutions & System Integration PLC Programming Services Professional PLC Programming & Automation Solutions - Ikode Automation is one of the best PLC programming and industrial automation solution... View product → |
 | Industrial Automation Solutions & System Integration Industrial Automation Component Sales Reliable Automation Components. Trusted Industrial Solutions.Ikodeautomation is one of the leading industrial automation component sellers and... View product → |
 | Industrial Automation Solutions & System Integration HMI Programming Services Ikodeautomation is one of the best HMI programming and industrial automation solution providers, offering professional HMI development and PLC-HMI... View product → |