
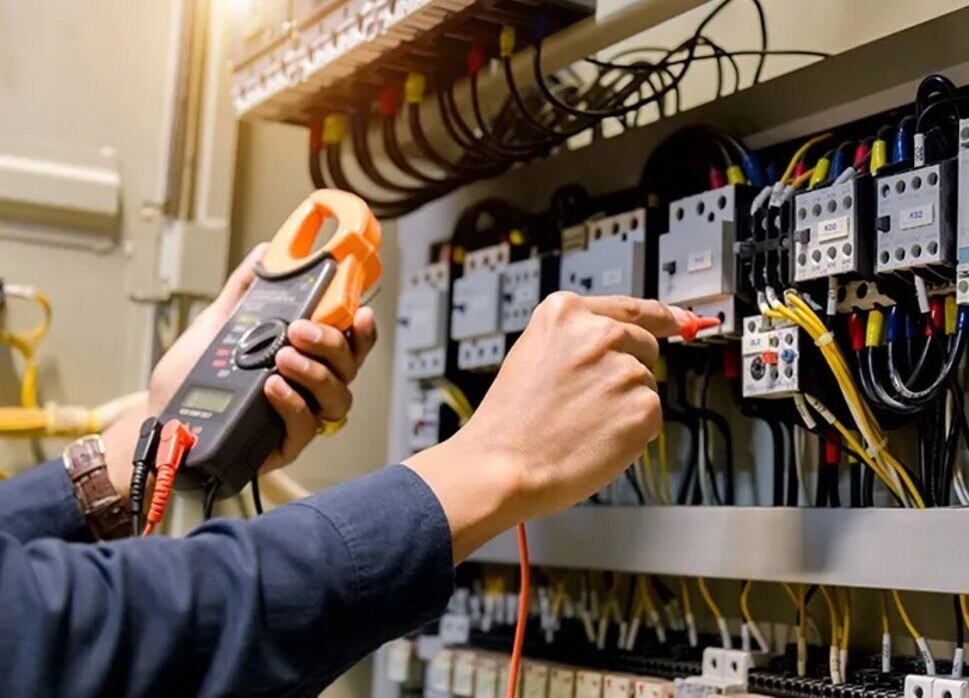
An AMC visit should produce evidence about the condition of your panels, controllers, drives, networks and operator systems—not just a statement that the PLC is running. By the end, you should know what the technician checked, what required isolation, which defects threaten production or safety, and what the contract includes next.
Key takeaways
- Send the asset register, failure history and production limits before arrival.
- Require safe isolation before inspecting panels or field hardware.
- Test PLC, network, VFD, HMI and SCADA backups during the visit.
- Demand documented faults, corrective work, test results and next actions.
Before the technician arrives: records, scope and production constraints
Provide the technician with the asset register, failure history and production limits before the visit. Without these records, an industrial automation maintenance contract can promise periodic attendance while leaving the actual equipment, software and response obligations undefined.
1. Send the current list of PLCs, HMIs, SCADA servers, VFDs, remote I/O, networks, panels and safety devices. Include electrical drawings, I/O lists, alarm history, VFD parameter files, PLC and HMI project backups, approved software versions, previous breakdown reports, open defects and the last backup date.
2. State which machines may stop, for how long, and during which shifts. Identify batch deadlines, continuous processes, clean-down windows, restricted areas and production states that make testing unsafe or impossible.
3. Confirm the contract scope, response target, restoration target, out-of-hours escalation and local critical spares. Define whether emergency work, shutdown projects and replacement parts are billable.
4. Establish remote-access rules before anyone connects. Record who authorizes access, which VPN or jump host is used, how sessions are logged and whether online edits are permitted.
Before touching equipment, the technician should agree the work order, affected assets, approved baseline and isolation boundary with operations and safety personnel. The technician must also identify forced bits, bypasses, undocumented online edits, changed scaling constants and mismatched HMI tags so a superficial “healthy” screen does not conceal a later failure.
The walkdown: panel condition, field hardware and safe isolation
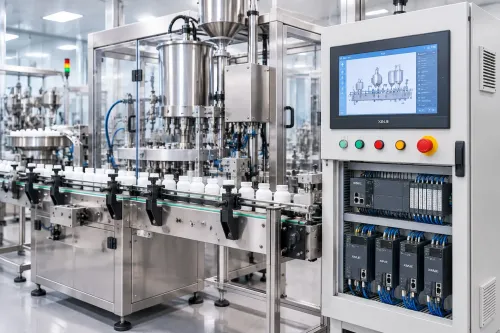
Production must stop before anyone opens an energised panel, tightens terminals, replaces a module, rewires a network, changes firmware, or tests a safety device. The technician first confirms the machine state, permit requirements and isolation boundary with the operator.
1. Walk around the asset and compare its identity with the asset register. Check guards, emergency stops, junction boxes, cable glands, conduit, exposed conductors, oil or water ingress, corrosion and signs of impact.
2. Inspect the control panel with the door closed, then open it only after authorised isolation. Look for loose terminals, discoloured wiring, damaged ferrules, missing labels, overheated contactors, blocked filters, failed cooling fans, dust, moisture, corrosion and abnormal cabinet temperature.
3. Check power supplies, UPS indicators, PLC battery and fan status, drive condition, spare modules and removable media. Record observed defects; cleaning without measured findings is not a maintenance result.
4. Review field hardware against the drawings and I/O list. Confirm sensor mounting, actuator connections, solenoid condition, cable damage, earthing and enclosure seals. Do not defeat a guard switch, emergency stop, permissive or trip to prove operation.
For intrusive work, apply lockout/tagout, isolate electrical, pneumatic, hydraulic and mechanical energy, then verify zero energy before touching equipment. Test safety functions only under an approved procedure that defines the expected safe state, reset behaviour and evidence to retain.
A provider handling automation equipment maintenance in Bengaluru should also document which findings need an immediate shutdown, which can wait for a planned window, and which trigger billable emergency work.
Online health checks for PLCs, networks and VFDs
A technician can assess controller, communication and drive health during production by reading diagnostics rather than changing the running system. The technician records a baseline, then compares it with the approved PLC and HMI/SCADA application versions before making any change.
- Controller mode, scan time, processor faults, power-supply status, battery condition and I/O diagnostics
- Live I/O values against the approved I/O list, including unexpected states and stale values
- Managed-switch port errors, duplex mismatches, link flaps, ring or redundancy status and duplicate IP addresses
- Network time synchronisation, unused ports, remote-access paths and separation from business networks
- VFD fault history, alarm codes, run hours, output current, speed reference and communication status
- Online edits, forced bits, bypassed permissives, altered scaling constants and mismatched HMI tags
These checks form part of industrial control system maintenance and usually leave the process running. A technician should not clear evidence before recording it; resetting a drive or deleting a diagnostic log can hide the cause of an intermittent stoppage.
Terminal tightening, module replacement, firmware work, network rewiring and safety-device testing require an approved shutdown, permit and lockout/tagout. The technician must isolate and verify hazardous energy before intrusive work, then document every finding for corrective action rather than treating a clean CPU status as proof that the system is healthy.
HMI, SCADA and backup testing: proving the system is recoverable
A proper PLC, HMI and SCADA check verifies recoverability, not just whether screens open and values appear. The technician compares the running logic and applications with the approved version, looking for undocumented online edits, forced bits, bypassed permissives, changed scaling constants and mismatched HMI tags.
These hidden differences can cause a failed sequence or unsafe restart.
During an AMC visit, ask the technician to verify:
- PLC diagnostics, I/O faults, communication status and controller clock against the approved baseline.
- HMI tag quality, engineering units, faceplate commands, navigation and operator acknowledgements.
- SCADA alarm generation, shelving, stale alarms, alarm floods and event timestamps.
- Historian writes, trend continuity, data quality and gaps during a controlled test.
- Time synchronisation across PLCs, HMIs, SCADA servers and network equipment.
- Recovery of recipes, alarm databases and user configuration, not merely their presence on a disk.
A backup is evidence only when it is complete, identifiable by asset, version and date, and restorable. Capture PLC programs, HMI projects, SCADA applications, recipes, alarm databases, VFD parameters, network-device configurations and licence files where permitted.
Test a restore on compatible hardware or in a documented recovery environment, record dependencies, and confirm that the machine reaches a known safe state. A copied project file alone proves nothing. The close-out should record what was tested, what failed, where backups reside and who owns the next recovery action.
Corrective work, contract choices and the handover report
A defect is not closed because a technician reset an alarm. Classify it as an immediate safety or production risk, a latent defect, or a lifecycle recommendation, then record the affected asset tag, evidence, consequence, containment, corrective action, shutdown requirement, parts, owner and target date. Escalate safety risks before continuing production.
Choose the contract model against your actual exposure:
- Preventive AMC: scheduled inspections, diagnostics, backups and a visit report; state whether corrective labour, travel and parts are extra.
- Comprehensive AMC: include defined corrective labour, critical spares, response and restoration targets, escalation outside business hours, and shutdown-project boundaries.
- On-call support: specify hourly rates, minimum charges, remote-support rules and the point at which an emergency becomes billable work.
Remote access is not automatic in industrial automation AMC service in Bengaluru. Your industrial automation maintenance contract must name the authorizer, VPN or jump host, session-log method, permitted hours and whether online PLC or HMI changes are allowed.
Check local spare availability and engineers who know your installed OEM platform; proximity alone does not guarantee restoration.
At close-out, demand a signed report containing:
- Open and closed defects, evidence, risk, action and target date
- Measurements, fault-history extracts and alarm or historian findings
- Changes made, software versions, parameter files and backup locations
- Parts used, parts recommended and any shutdown requirement
- Technician, plant owner, approval and next-visit date
IkodeAutomation |08048033508 can be one local comparison point, but judge the provider by those documented commitments rather than a Bengaluru address.
Related product
 | Industrial Automation Solutions & System Integration PLC, HMI, SCADA & VFD Maintenance Industrial Automation AMC Services AMC Work – Annual Maintenance Contract Services-Reliable Industrial Automation Support for Uninterrupted Operations Ikodeautomation provides... View product → |
Frequently asked questions
What records should you provide before an industrial automation AMC visit?
Provide the asset register, failure history, control-system drawings, software and backup records, maintenance scope, and production constraints.
What does a technician inspect during the walkdown?
The technician checks panel condition, wiring, cooling, power supplies, field instruments, network hardware, VFDs and safe-isolation requirements.
How are PLCs, networks and VFDs checked while production continues?
Online checks review PLC diagnostics, processor status, communication faults, network health, drive alarms, operating values and recurring events without unnecessary shutdowns.
Why should HMI, SCADA and backup recovery be tested?
A backup is useful only when it restores the required PLC, HMI or SCADA system; testing exposes missing files, incompatible versions and failed recovery steps.
What should the AMC handover report contain?
Record observed faults, corrective work, parts used, test results, unresolved risks, recommended upgrades, response obligations and the next maintenance actions.